Email: info@touchsh.com
User
Municipal & Water Treatment Industry: Wall-mount Industrial All-in-One PC Realizes On-site Data Monitoring & Management
2026-10-13 17:01:20
9
Municipal & Water Treatment Industry: Wall-mount Industrial All-in-One PC Realizes On-site Data Monitoring & Management
[Shanghai, China — October 13, 2026] — Municipal water supply and wastewater treatment facilities are critical infrastructure — and they're increasingly going digital. To ensure water quality, meet regulatory standards, and operate efficiently, these facilities need reliable on-site data monitoring at every stage of the treatment process.
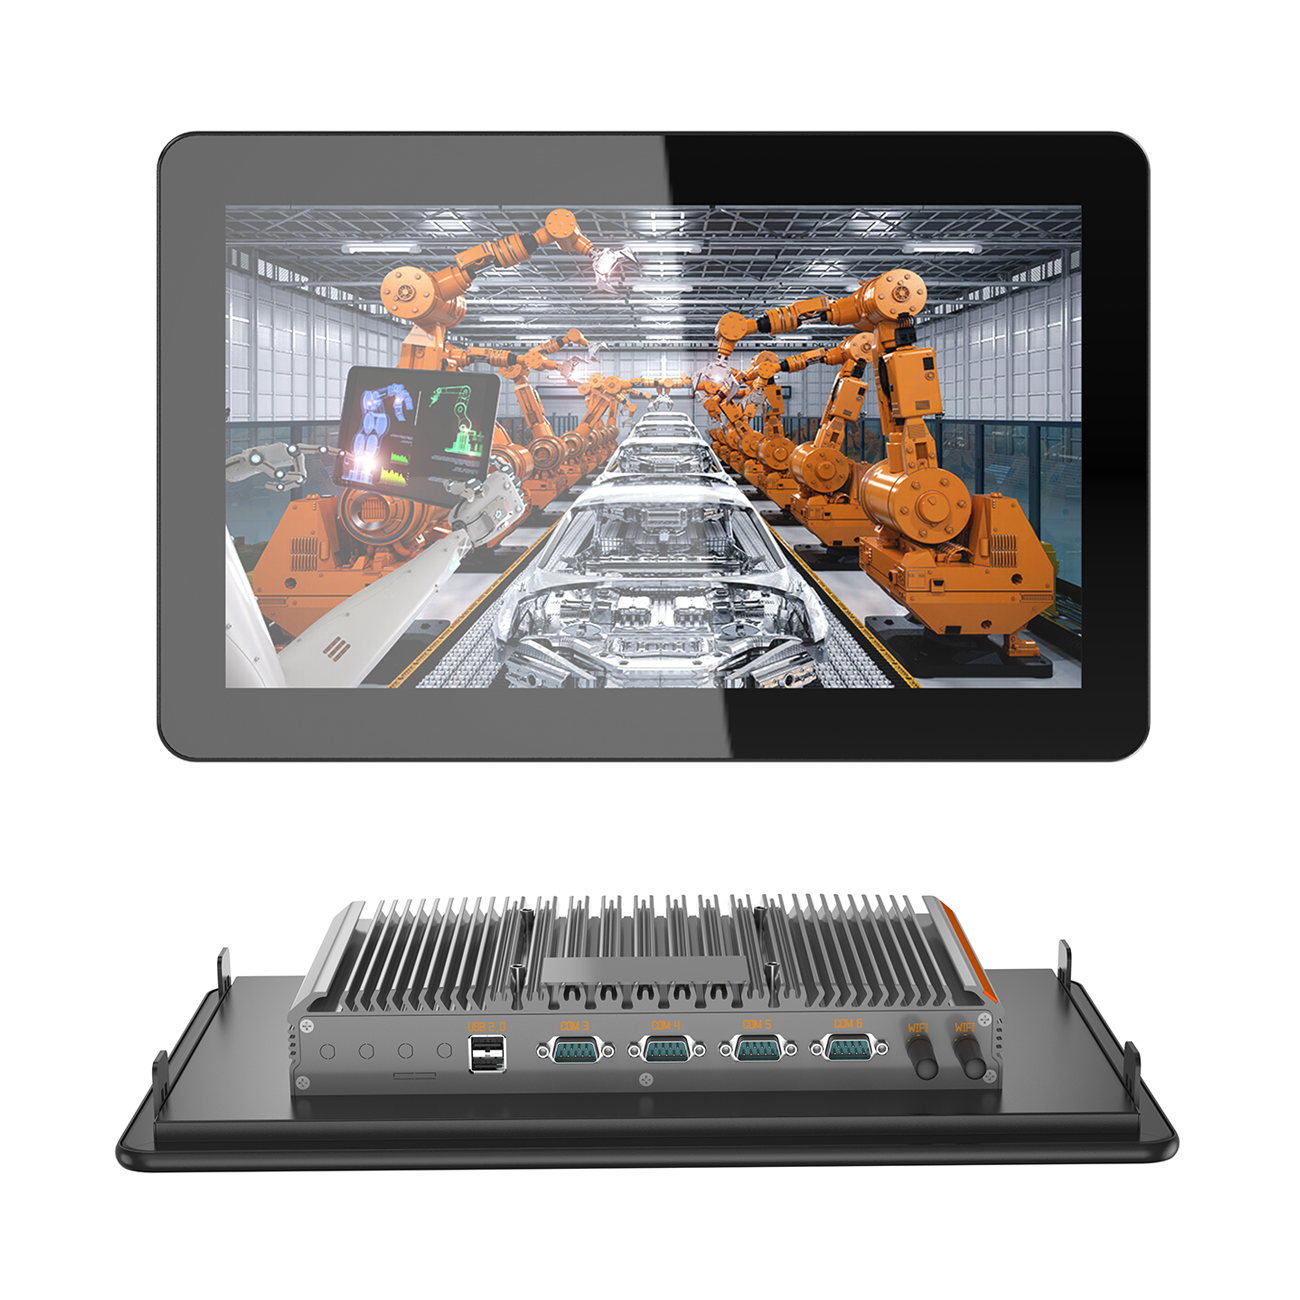
Wall-mount industrial all-in-one PCs have become the terminal of choice for these environments — rugged, fanless, network-connected, and seamlessly integrated with PLC/SCADA systems. Mounted on walls near equipment, they provide operators with real-time data visualization, alarm management, and local control — right where it's needed.
Why Water Treatment Needs Wall-mount Industrial PCs
Water treatment facilities present unique challenges for computing equipment:
- Humidity and moisture — treatment areas are inherently wet, with splashing, condensation, and high humidity
- Chemical exposure — chlorine, coagulants, disinfectants, and cleaning agents create corrosive atmospheres
- Space constraints — pump rooms, control panels, and equipment areas have limited floor space
- 24/7 operation — water treatment never stops; terminals must run continuously
- Regulatory compliance — accurate data logging and reporting are legally required
- Remote locations — pump stations and pipeline monitoring points may be unmanned and remote
- Wet-hand operation — operators often have wet or gloved hands when interacting with terminals
Consumer PCs and office-grade equipment fail quickly in these conditions. Wall-mount industrial all-in-one PCs are engineered specifically for them.
Key Capabilities for Water Treatment On-site Monitoring
1. Fanless IP65 Rugged Construction
- No ventilation openings — no moisture or chemical ingress, zero maintenance
- IP65 front panel — dust-tight, splash-resistant, suitable for wet treatment areas
- Conformal coating on internal PCBs — protection against humidity and chemical vapors
- Solid-state storage — no moving parts, vibration-resistant
- 100,000+ hour MTBF — reliable 24/7 operation
2. Wall-mount Installation
- Saves valuable floor space in pump rooms and control areas
- Mounts at ergonomic height for operator access
- Protects equipment from accidental impact, water splash, and dust
- Clean, organized installation with cable management
- Panel mount and VESA wall-mount options available
- Sizes from 7" to 27" — fit any wall space
3. Capacitive Multi-Touch with Wet/Gloved Operation
- PCAP 10-point capacitive touch — fast, accurate response
- Enhanced controllers support wet-finger and thin-glove operation
- Water-rejection algorithms — reliable even with water droplets on screen
- High-brightness display option (1000+ nits) for bright environments
- Anti-glare coating option for reduced reflection
4. Rich Connectivity for PLC/SCADA Integration
- RS232/RS485 — connect to PLCs, instruments, flow meters, level sensors, analyzers (Modbus RTU)
- Ethernet (Gigabit) — connect to SCADA systems, plant network, remote access (Modbus TCP, OPC UA)
- USB — connect to barcode scanners, printers, backup storage
- GPIO — connect to alarms, indicators, pump control signals
- Optional 4G LTE — for remote pump stations and pipeline monitoring where wired network is unavailable
- Protocol support — Modbus RTU/TCP, OPC UA, MQTT for seamless SCADA integration
5. On-site Data Monitoring & Management Software
- Real-time process data visualization (flow, pressure, level, pH, turbidity, chlorine residual)
- Local alarm management with visual/audio alerts and acknowledgment
- Historical trend analysis and data logging for regulatory compliance
- Recipe and setpoint management for chemical dosing
- User access control and operation logging
- Remote monitoring and control via network
Key Application Scenarios
| Application | Wall-mount Industrial All-in-One PC Role |
|---|---|
| Water Treatment Plants | SCADA HMI terminal, process visualization, alarm management, operator control |
| Wastewater Treatment | Activated sludge process control, aeration monitoring, sludge level management, effluent quality display |
| Pump Stations | Pump status monitoring, level control, pressure monitoring, fault alarm, remote 4G connectivity |
| Chemical Dosing | Dosing rate control, chemical level monitoring, flow pacing, alarm management |
| Filtration Systems | Filter status, backwash control, pressure differential monitoring, flow management |
| Pipeline Networks | Pressure monitoring, flow measurement, leak detection alarm, remote data logging |
| Water Quality Monitoring | pH, turbidity, chlorine, DO, conductivity real-time display, compliance reporting |
| Reservoir & Intake | Level monitoring, water quality display, pump control, remote communication |
Benefits for Municipal & Water Treatment Operations
- Real-time visibility — operators see process data instantly, enabling faster response to issues
- Regulatory compliance — accurate data logging and reporting meet environmental standards
- Reduced manual inspection — on-site monitoring reduces the need for routine manual rounds
- Faster fault response — local alarms alert operators immediately to pump failures, level anomalies, or quality issues
- Lower downtime — fanless rugged design means fewer failures and zero maintenance
- Improved efficiency — data-driven process optimization reduces chemical and energy consumption
- Remote management — network connectivity enables central monitoring of distributed pump stations
Senke Wall-mount Industrial All-in-One PCs for Water Treatment
Senke's industrial all-in-one PC lineup is engineered for municipal and water treatment on-site monitoring:
- Sizes: 7" to 27" — from compact pump station terminals to large control room displays
- Construction: Fanless, IP65 front panel, conformal coating option, solid-state storage
- Mounting: Wall-mount (VESA), panel mount, desktop stand — flexible installation
- Touch: PCAP 10-point capacitive, wet-finger/gloved capable, anti-glare option
- Display: 350 nits standard, 1000–1500 nits high-brightness option
- I/O: RS232/RS485, Gigabit Ethernet, USB, GPIO, HDMI
- Wireless: Dual-band Wi-Fi, Bluetooth 4.2, optional 4G LTE (for remote stations)
- OS: Android 11, Linux, Windows 10/11 IoT
- Protocols: Modbus RTU/TCP, OPC UA, MQTT
- Reliability: 100,000+ hour MTBF, 7–10 year lifecycle
- Customization: OEM/ODM for branding, I/O, enclosure, software integration
Conclusion
Municipal water supply and wastewater treatment facilities depend on reliable on-site data monitoring to ensure water quality, regulatory compliance, and operational efficiency. Wall-mount industrial all-in-one PCs — with fanless IP65 construction, wall-mount installation, wet/gloved touch capability, rich PLC/SCADA connectivity, and 24/7 reliability — deliver the rugged, network-connected monitoring terminals that water treatment environments demand.
From water plants and wastewater treatment to pump stations, chemical dosing, filtration systems, and pipeline networks, these wall-mount terminals provide real-time data visualization, local alarm management, and remote access — helping facilities operate more efficiently, comply with regulations, and minimize downtime.
As municipal infrastructure continues to modernize, wall-mount industrial all-in-one PCs will remain the foundation of on-site data monitoring and management in the water treatment industry. Senke's comprehensive lineup — with fanless IP65 construction, rich connectivity, multiple OS options, and full customization — is the ideal choice for municipal and water treatment applications worldwide.
About Senke Senke is a trusted global provider of industrial display solutions, touch computers, and HMI systems. With a full lineup from 7" to 27" — featuring fanless IP65 construction, wall-mount/panel-mount options, capacitive multi-touch with wet/gloved operation, rich industrial I/O (RS232/RS485/Ethernet/GPIO), optional 4G LTE for remote sites, Modbus/OPC UA/MQTT protocol support, and multiple OS options — Senke delivers wall-mount industrial all-in-one PCs engineered for reliable on-site data monitoring and management in municipal and water treatment applications. Comprehensive OEM/ODM customization and 7–10 year lifecycle commitment make Senke the ideal partner for water treatment digitalization worldwide.
Contact Senke International Sales Department Email: sales@senke.com Website: www.senke.com
New News
Hot Products
Full Screen Digital Advertising Poster
Ultra-thin 4k
10 Inch Windows Rugged Tablet
Android 11,MT8788,4G,64G
Senke Electronic is a manufacture of industrial panel pc, industrial box pc, rugged tablet, kiosk payment and digital display advertising.